
Custom Pharmaceutical-Grade Vial Labels
In the pharmaceutical industry, a vial label is never just about affixing a product name to a package.
It bears multiple responsibilities, including drug identity verification, usage safety warnings, traceability management, and compliance auditing.
The removal, blurring, or incorrect information on a label can directly lead to medication errors or even trigger serious medical incidents.
Therefore, our requirements for each label extend far beyond mere aesthetics; we strive for absolute reliability under extreme conditions and for professional empowerment within compliance frameworks.
1. Starting with label Materials: Engineered for Pharmaceutical Environments
The storage and transportation environments for pharmaceutical products are highly complex, ranging from cold chain warehousing at- 20 °C to liquid nitrogen environments, through repeated freeze–thaw cycles, to condensation exposure during ambient-temperature transportation.
Under such conditions, conventional labels are often susceptible to issues such as lifting, delamination, discoloration, or blurred text.
We use specialized silver/hologram silver waterproof material for vial labels that are designed specifically for harsh pharmaceutical storage environments.
Exceptional weather resistance:
Suitable for low-temperature storage (-20°C to -80 °C), repeated freeze–thaw cycles, and high-humidity environments; the vial labels will not peel off or curl.
Excellent chemical resistance:
Resistant to alcohol wiping and disinfectant corrosion; suitable for the packaging of various pharmaceutical products.
Waterproof and moisture-resistant:
Even when significant condensation occurs during cold-chain transportation, the vial label information remains clearly legible, and the barcode/QR code can still be scanned normally.

We have combined high-precision color printing with a metallic finish substrate to achieve these effects:
High-contrast display:
Highlighting for enhanced readability:


Vial labels meet the stringent requirements of the pharmaceutical industry
We are fully aware that pharmaceutical labels serve not only end-users but also must comply with the stringent requirements imposed by regulatory authorities and across all segments of the supply chain. Our label printing content can include the following:
Barcode/QR code:
High-precision printing ensures full traceability throughout the entire supply chain.
Expiry date and batch number:

In the pharmaceutical industry, trust is built upon every detail.
Make our labels the first testament to the reliability of your products.
Please feel free to contact us to request samples or learn about industry application cases;
We look forward to providing you with professional labeling solutions for your pharmaceutical products.
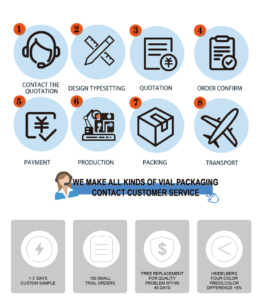
Order Process
Payment
Logistics and Transportation


Reviews
There are no reviews yet.